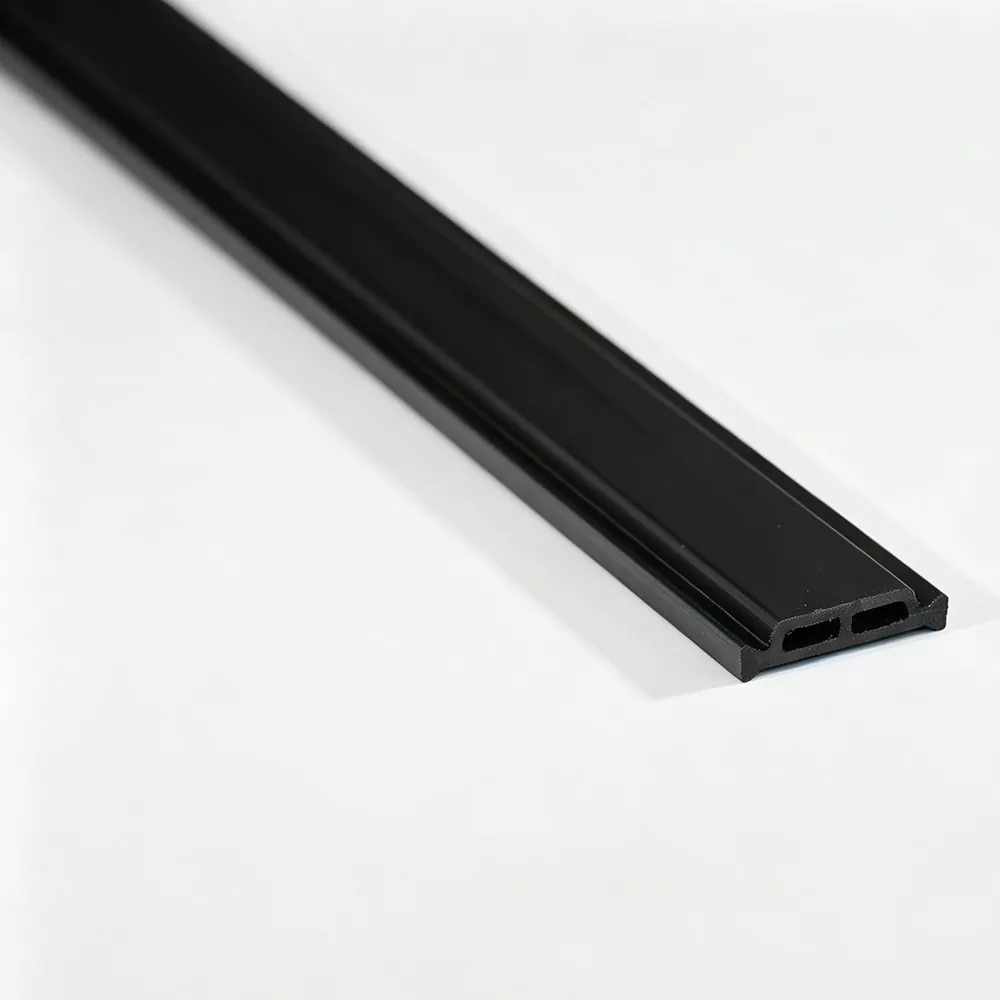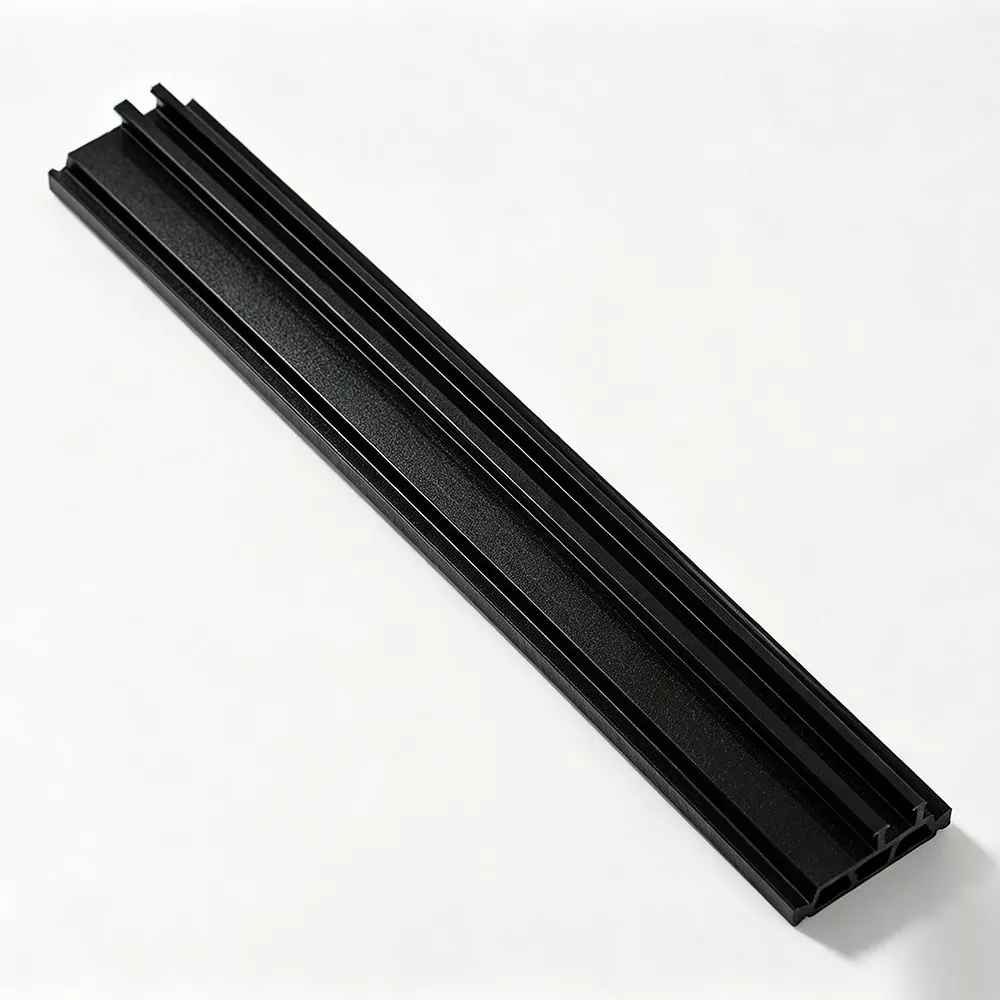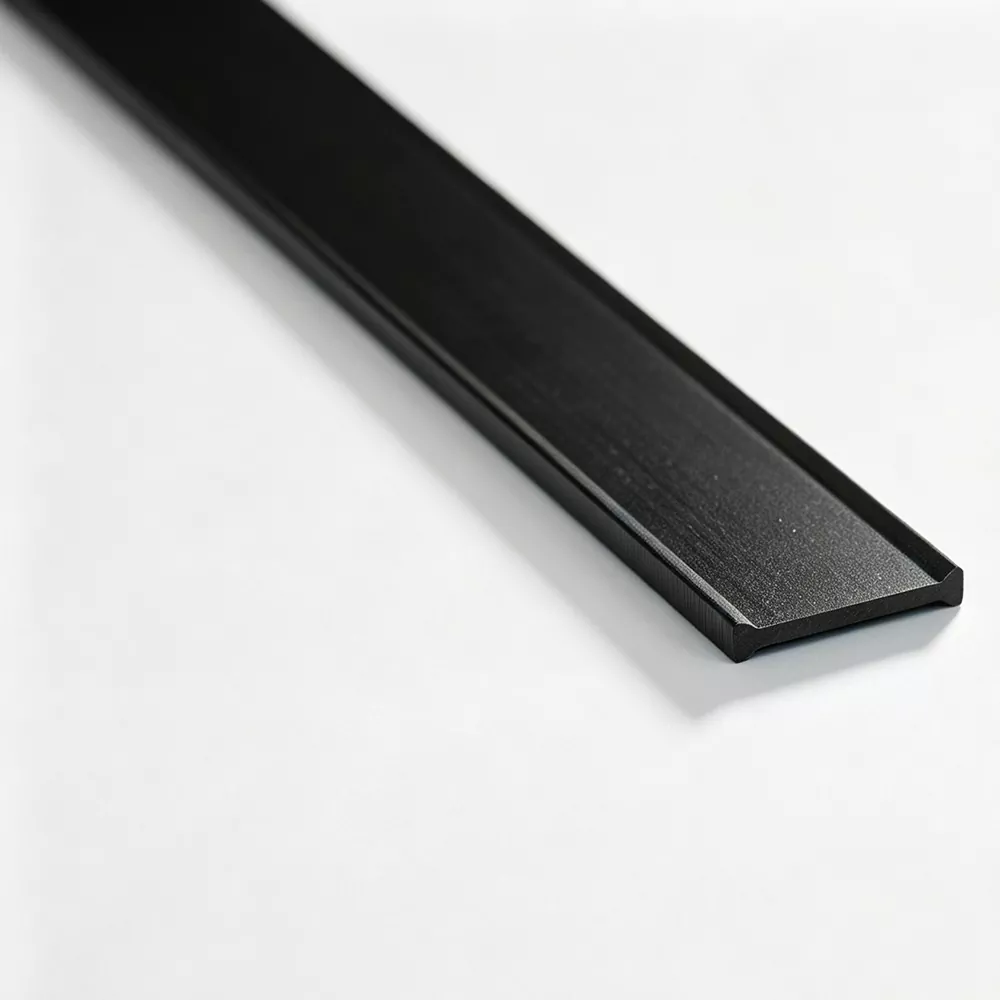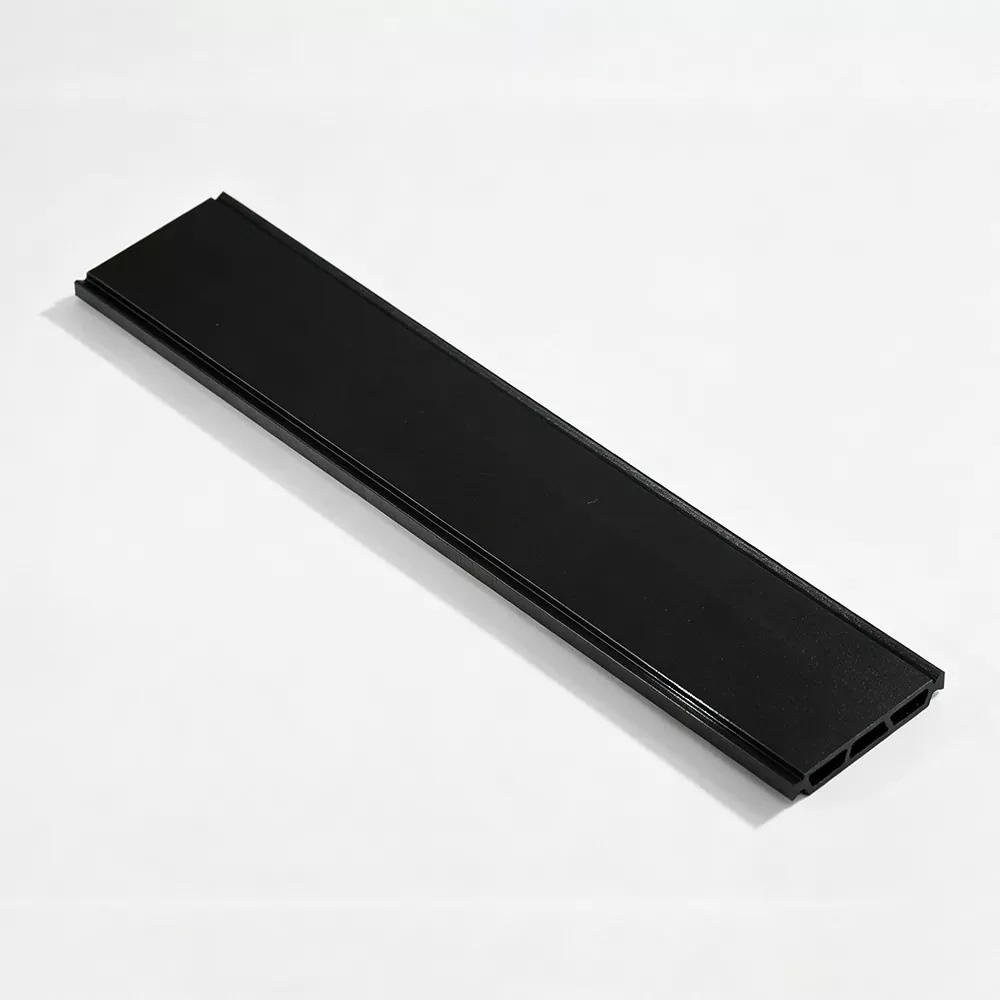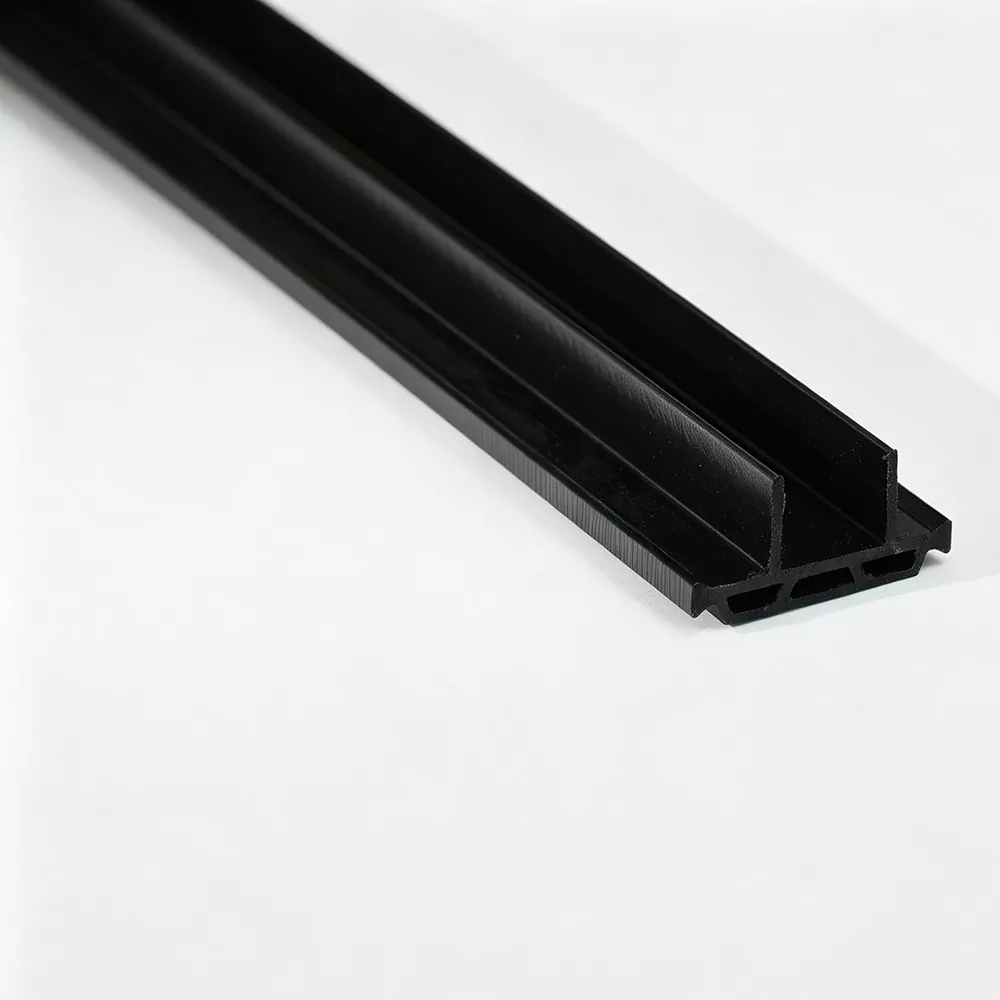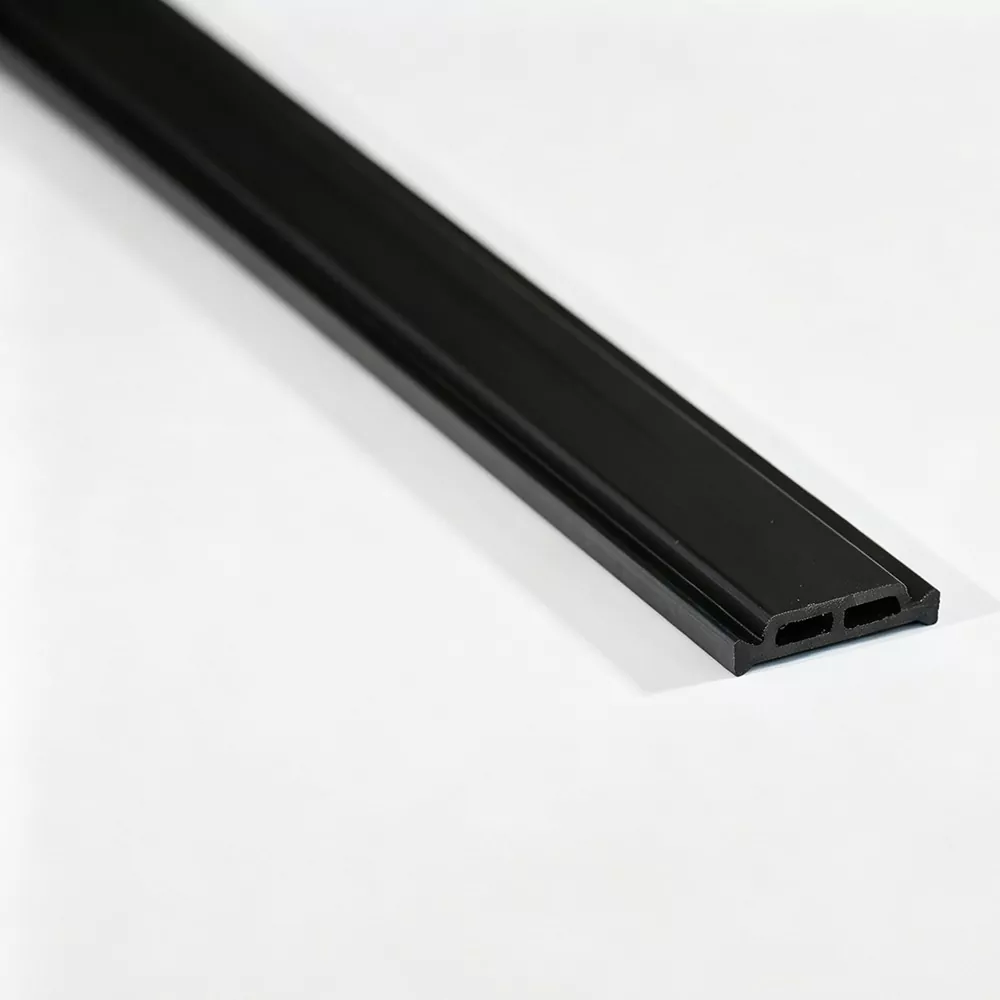
PA66 GF25 Thermal Break Strips are reinforced polyamide profiles used to separate interior and exterior aluminum sections in thermally broken window, door, and curtain wall systems. Their performance depends on more than the nominal material grade. Glass-fiber distribution, cross-sectional geometry, dimensional accuracy, mechanical strength, and compatibility with the aluminum cavity all influence the finished assembly. This guide explains how the material works, how common profile shapes differ, which dimensions should be checked, how extrusion and quality inspection affect consistency, and what technical information is useful when developing a profile for a specific aluminum system.
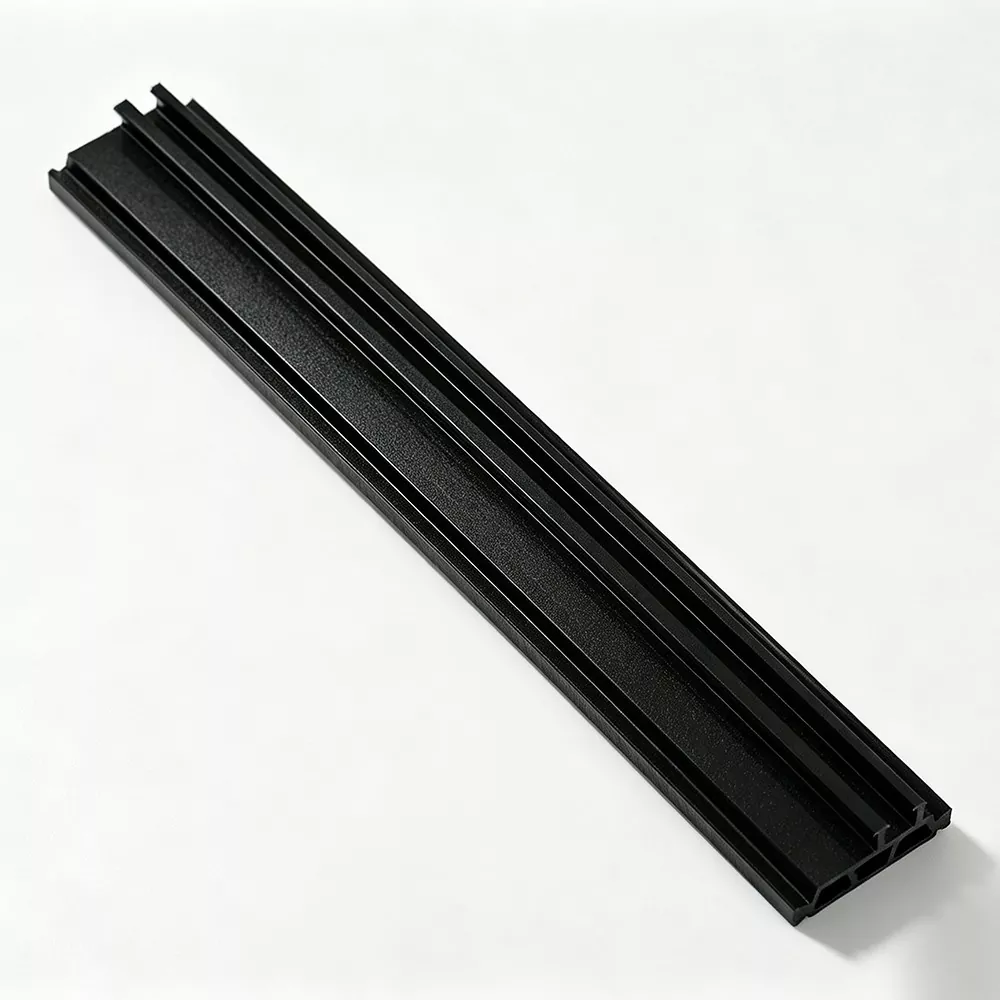
Table of Contents
Explore the Guide- 01What Is the Material?
- 02PA66 and Glass-Fiber Composition
- 03How Thermal Separation Works
- 04Mechanical and Dimensional Properties
- 05Common Cross-Section Types
- 06Matching Strips to Aluminum Profiles
- 07Manufacturing and Extrusion
- 08Quality Inspection and Testing
- 09Typical Applications
- 10Customized Profile Development
- 11Practical Selection Checklist
- 12Frequently Asked Questions
01What Is a PA66 GF25 Thermal Break Profile?
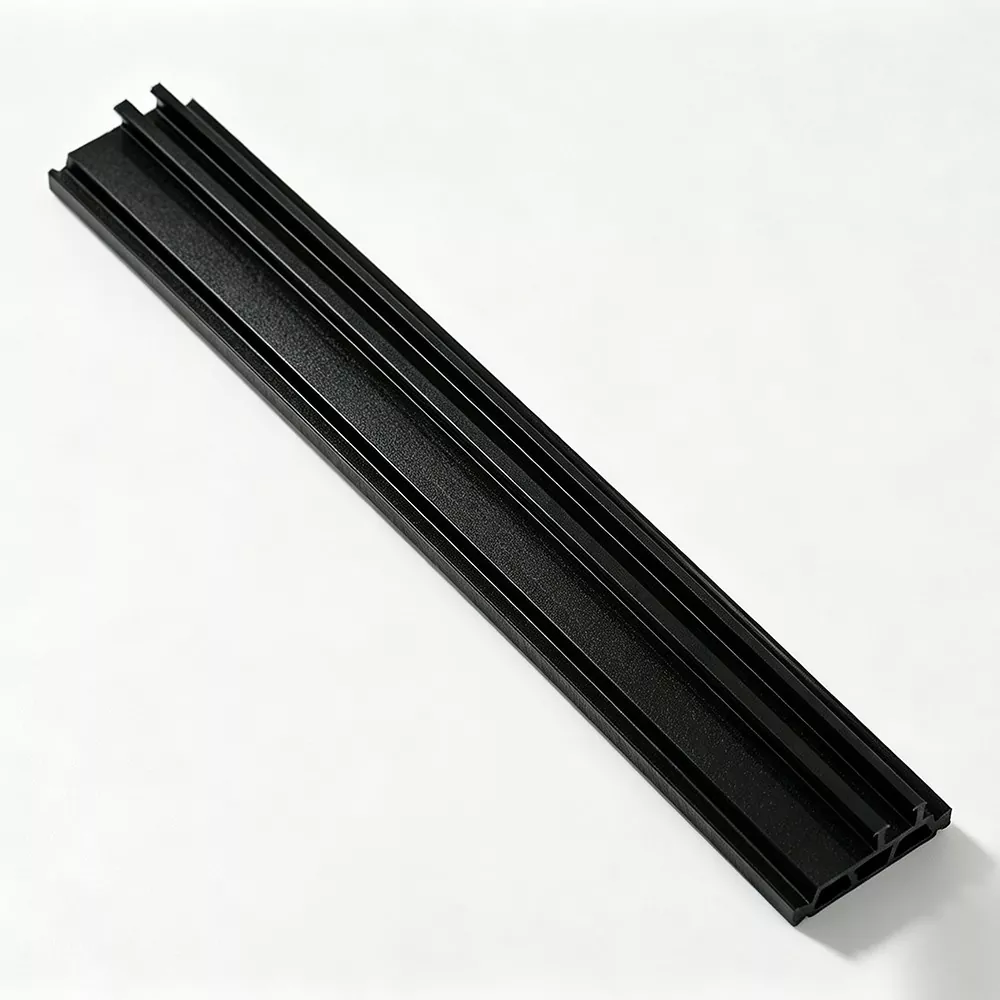
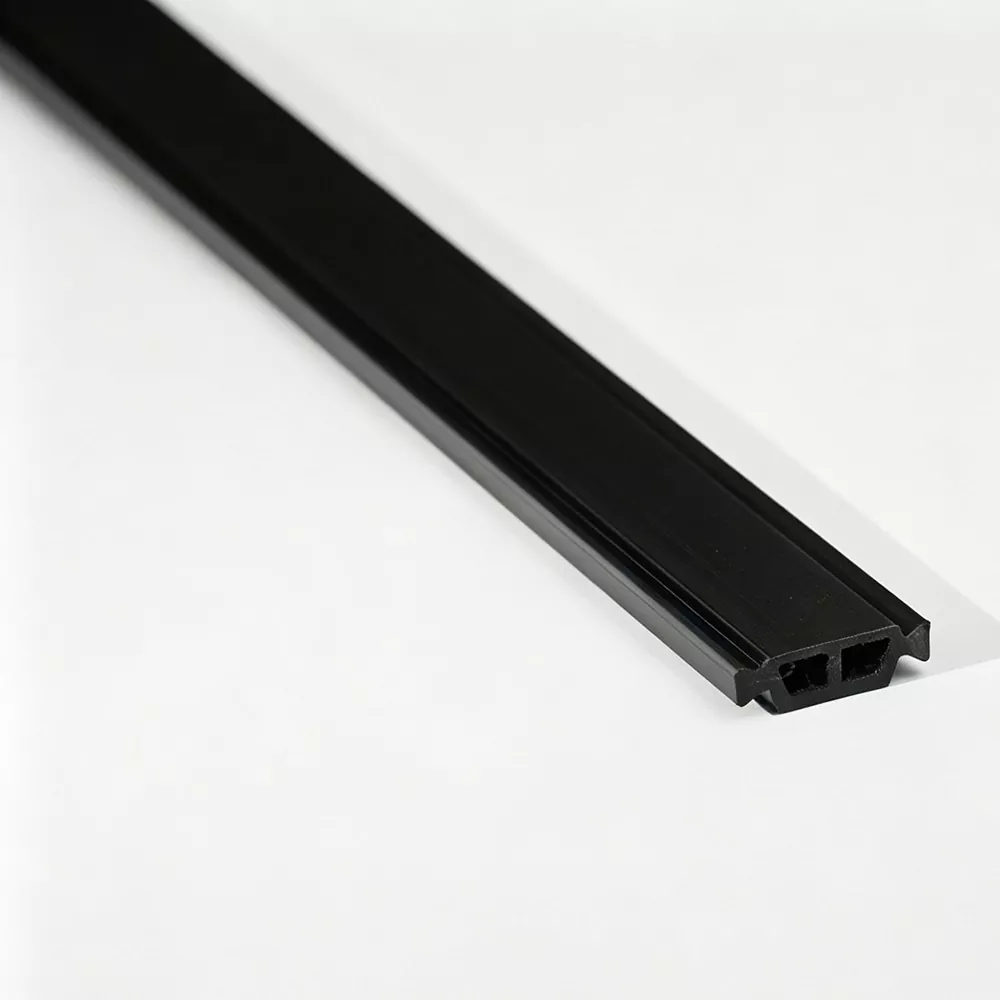
A thermal break profile is a non-metallic component installed between separate aluminum sections to interrupt the direct heat-transfer path through a metal frame.
Aluminum is widely used in architectural frames because it is lightweight, workable, and structurally useful. However, aluminum also conducts heat readily. When the interior and exterior parts of an aluminum frame remain directly connected, heat can travel through the frame more easily. A thermal break creates a separation between these metal sections and changes the way heat moves through the assembled profile.
Polyamide is commonly selected for this role because it combines insulating characteristics with mechanical properties suitable for profile assembly. Reinforced grades are used where the strip must maintain its shape and remain securely engaged with the aluminum during insertion or rolling operations.
The product is not simply a plastic spacer. Its cross-section must be designed to fit the aluminum cavity, engage with the grooves, and withstand the forces generated during manufacturing and service. A suitable profile therefore needs both material consistency and precise dimensional control.
02Understanding PA66 and 25% Glass-Fiber Reinforcement
PA66, also known as polyamide 66 or nylon 66, is an engineering thermoplastic used in components that require a combination of strength, stiffness, and dimensional control. The GF25 designation indicates that the compound contains 25% glass fiber by weight. These fibers reinforce the polymer matrix and modify its mechanical behavior.
Why Is PA66 Used?
PA66 offers a useful balance of mechanical strength, heat resistance, and processability for engineered profiles. Its properties make it suitable for components that must retain a defined shape while being handled, assembled, and exposed to changing environmental conditions.
For thermal break applications, material selection should consider the complete processing and service environment. Moisture conditioning, temperature exposure, profile dimensions, and assembly forces can all influence the behavior of a polyamide component.
What Does GF25 Add?
Glass fibers increase stiffness and help improve dimensional stability compared with an unreinforced polyamide compound. Reinforcement is particularly relevant when a long, narrow profile must resist deformation during handling and aluminum profile assembly.
Higher Rigidity
Glass-fiber reinforcement increases stiffness, helping the profile maintain its designed cross-section during processing and installation.
Dimensional Control
The reinforced compound supports more stable profile dimensions when extrusion and cooling conditions are properly controlled.
Mechanical Engagement
Appropriate strength and stiffness help the strip remain engaged with aluminum grooves during insertion and roll-forming.
Directional Properties
Fiber orientation influences longitudinal and transverse behavior, making extrusion design and process control important.
The glass-fiber percentage alone does not describe every performance characteristic. Two compounds with the same nominal reinforcement level may behave differently because of resin quality, fiber length, fiber distribution, moisture condition, and processing history. Technical evaluation should therefore include both material information and finished-profile test results.
03How Does Thermal Separation Work in Aluminum Frames?
Thermal separation works by replacing a continuous metal connection with a lower-conductivity section. In a thermally broken frame, the interior and exterior aluminum components are separated by polyamide profiles. This interrupts the direct conductive path that would otherwise extend through the aluminum frame.
Interrupting the Metal Heat-Transfer Path
Heat moves through materials according to their thermal properties and the geometry of the assembly. Aluminum conducts heat much more readily than polyamide. Introducing a polyamide section between two aluminum parts therefore changes the heat-flow route through the frame.
The width of the insulating section, the profile shape, and the surrounding metal geometry all contribute to the thermal behavior of the finished system. A wider thermal break may provide a longer path through the insulating material, but width should not be considered in isolation. The complete frame design must be evaluated.
Why the Complete Window System Matters
A thermal break strip cannot determine the thermal performance of an entire window or curtain wall by itself. Glazing configuration, frame depth, air leakage, weather seals, drainage design, hardware, and installation details also matter. The strip is an important component within a larger engineered assembly.
04Mechanical Strength and Dimensional Stability
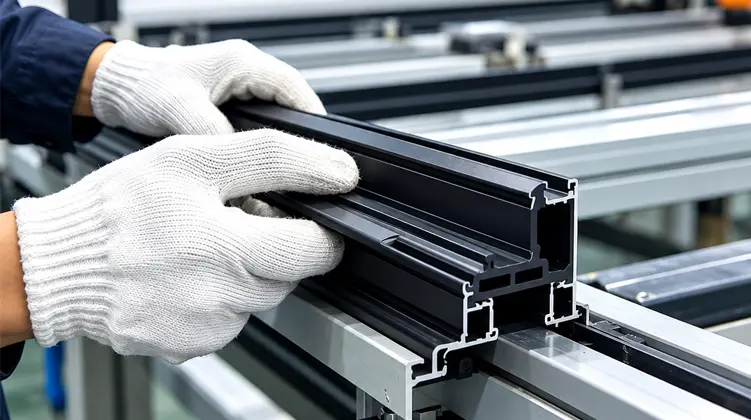
Mechanical performance is essential because a thermal break profile must do more than separate two aluminum sections. It must also remain securely connected to them. During assembly, the strip may experience insertion pressure, rolling forces, friction, and localized stress around its locking features.
Longitudinal Tensile Strength
Longitudinal tensile strength describes resistance to pulling forces along the length of an extruded strip. It is relevant when profiles are handled, transported, inserted, or processed through equipment. Fiber orientation along the extrusion direction can influence this property.
Transverse Shear Resistance
Transverse strength is important because forces applied across the profile can affect the connection between the polyamide strip and aluminum sections. The locking geometry, groove dimensions, material condition, and roll-forming process all contribute to the mechanical integrity of the assembled profile.
Dimensional Stability
Dimensional stability concerns the ability of a profile to maintain its intended shape and measurements. Width, height, wall thickness, and locking features must remain within the agreed tolerances so that the strip can fit the aluminum cavity consistently.
Changes in moisture content and temperature can affect polyamide dimensions and mechanical behavior. Storage, conditioning, and production environments should be considered when defining inspection methods and assembly requirements.
- Check longitudinal tensile properties for handling and processing requirements.
- Review transverse strength and shear behavior for the intended locking structure.
- Confirm width, height, thickness, and critical cross-sectional dimensions.
- Consider moisture conditioning and temperature exposure during evaluation.
- Assess the profile after the intended insertion or rolling process.
05Common Cross-Section Types and Their Uses
Thermal break profiles are available in different cross-sectional configurations. The correct type depends on the shape of the aluminum cavity, the locking structure, and the production method used to join the metal sections.
I-Type Profiles
I-Type profiles generally have a relatively straight-sided section and are used with compatible straight-groove aluminum cavities. Their suitability depends on the dimensions and engagement features of the specific extrusion. The strip must fit securely without excessive insertion force or unwanted movement.
C-Type Profiles
C-Type profiles have a shaped cross-section intended for compatible curved, stepped, or specially formed aluminum cavities. The geometry can help create a defined mechanical engagement when the aluminum groove is designed for that section.
T-Type Profiles
T-Type profiles use a head-and-stem configuration. The wider head and narrower connecting section must correspond with the receiving groove and the assembly requirements of the aluminum profile. Accurate matching is important to avoid interference during insertion and rolling.
Special-Shaped Profiles
Some aluminum systems use cavities that cannot be matched with a standard profile shape. Special-shaped sections can be developed around a drawing, dimensional specification, or physical profile information. The design should account for the full cross-section, including locking details and any local thickness changes.
| Profile Type | Typical Structural Feature | Main Matching Consideration |
|---|---|---|
| I-Type | Generally straight-sided cross-section | Compatibility with straight grooves and cavity dimensions |
| C-Type | Curved or stepped engagement geometry | Matching the aluminum cavity shape and locking area |
| T-Type | Head-and-stem configuration | Matching head width, stem dimensions, and groove opening |
| Special-Shaped | Custom cross-section for a particular extrusion | Drawing accuracy, assembly method, and functional dimensions |
Profile names are useful for initial classification, but they are not enough to confirm compatibility. Manufacturers should compare actual cross-sectional drawings and critical dimensions before selecting a type.
06How to Match the Strip with an Aluminum Profile
Matching the thermal break to the aluminum extrusion is one of the most important stages of product selection. A profile that looks similar to the required section may still have an unsuitable locking feature, width, or height. The receiving cavity should be treated as the starting point for selection.
PA66 GF25 Thermal Break Strips should be assessed against the aluminum profile drawing and the actual assembly process, rather than selected by product name alone.
| Aluminum Profile Detail | Strip Dimension or Feature | What to Verify |
|---|---|---|
| Cavity width | Strip width | Fit, engagement, and dimensional tolerance |
| Cavity depth | Profile height | Correct seating within the aluminum section |
| Groove structure | Locking geometry | Compatibility with insertion and roll-forming |
| Required separation | Strip thickness and section design | Available space and system configuration |
| Assembly equipment | Profile tolerances and engagement details | Insertion force, rolling conditions, and stability |
| Supply and processing method | Length and supply form | Compatibility with cutting, handling, and production lines |
Check the Complete Cross-Section
Width and height are only two parts of the dimensional review. The groove opening, locking shoulders, wall thickness, corner radii, and local transitions may also affect fit. Small differences in these areas can change insertion resistance or the way the strip locks into the aluminum.
Consider the Assembly Method
Insertion and rolling processes place different demands on the profile. A section that fits the cavity dimensionally may still be difficult to process if the locking geometry or surface condition is unsuitable. Evaluation should therefore include the intended equipment and production parameters.
07Manufacturing Processes Behind Consistent Profiles
Extrusion manufacturing transforms a reinforced polymer compound into a continuous profile with a defined cross-section. Stable production requires control of incoming materials, compounding conditions, extrusion parameters, cooling, shaping, and cutting.
Raw Material Preparation
PA66 resin and glass fiber are the principal materials in the reinforced compound. Incoming material checks may include melt flow index, glass-fiber content, and moisture condition. These factors influence melt behavior, fiber distribution, and the consistency of the finished profile.
Moisture control is particularly important when processing polyamide. Material handling and drying procedures should be appropriate for the resin and the production conditions. Incorrect preparation can affect surface appearance and processing stability.
Twin-Screw Extrusion
Twin-screw extrusion is used to process and shape reinforced thermoplastic compounds. The screw configuration and operating conditions influence material mixing, melt movement, and fiber distribution. A suitable die then forms the required cross-sectional geometry.
Cooling and Shaping
After leaving the die, the extruded profile passes through a controlled cooling and shaping process. Temperature, pulling speed, and cooling conditions influence dimensional stability. If these parameters are not balanced, the profile may show dimensional variation, deformation, or surface defects.
Fiber Orientation and Cutting
Glass-fiber orientation is affected by material flow through the extrusion system and die. It contributes to the directional mechanical properties of the finished profile. Once the section has been cooled and stabilized, precision cutting produces the required supply length.
- Material preparation: Check resin condition, glass-fiber content, and moisture before processing.
- Compound feeding: Maintain stable feeding and material blending conditions.
- Extrusion molding: Use the appropriate die and controlled extrusion parameters to form the section.
- Cooling and shaping: Stabilize the profile while controlling temperature and pulling speed.
- Dimensional inspection: Review cross-sectional dimensions and surface condition during production.
- Precision cutting: Cut the finished profile to the agreed supply length and inspect the final appearance.
For suitable specifications, straight strips may be supplied at 6 meters per piece, while compatible coiled profiles may be supplied at 500 meters per roll. The appropriate form depends on the section geometry, handling requirements, and downstream processing method.
08Quality Inspection and Important Test Items
Quality evaluation should cover material characteristics, dimensional accuracy, mechanical behavior, and the condition of the finished profile. A single test cannot represent every requirement of an aluminum thermal break system. Inspection criteria should be connected to the intended application and the technical specification agreed for the product.
Incoming Material Checks
Incoming inspection may review resin identification, melt flow behavior, glass-fiber content, and moisture. Consistent raw materials provide a more stable basis for extrusion and finished-profile control.
In-Process Inspection
During production, cross-sectional dimensions and surface condition can be checked at defined intervals. Recording process parameters helps identify variation and supports production traceability. Inspection points may include width, height, thickness, profile shape, and visible surface defects.
Laboratory Evaluation
Depending on the specification, laboratory testing can include density, Shore hardness, longitudinal and transverse tensile strength, water resistance, thermal aging, and linear expansion characteristics. The applicable test method and conditioning requirements should be defined before results are compared.
Finished Product Inspection
Before shipment, finished strips can be checked for appearance and dimensions. Packaging and handling should also protect the profile from bending, contamination, and unnecessary mechanical damage. An English inspection report can support technical communication and incoming quality review.
| Inspection Item | What It Evaluates | Why It Matters |
|---|---|---|
| Glass-fiber content | Reinforcement proportion in the compound | Supports material consistency and specification control |
| Dimensional inspection | Width, height, thickness, and cross-section | Confirms fit with the aluminum cavity |
| Shore hardness | Resistance to indentation under a defined method | Provides a material property for specification review |
| Tensile strength | Longitudinal and transverse mechanical behavior | Helps evaluate handling and assembly requirements |
| Water resistance | Behavior under defined moisture exposure | Supports evaluation for the intended service environment |
| Thermal aging | Property changes after defined heat exposure | Helps assess material stability under test conditions |
| Linear expansion | Dimensional change with temperature | Useful for considering profile fit across temperature changes |
Test results should be interpreted using the relevant method, specimen preparation, conditioning, and acceptance criteria. A meaningful quality specification identifies both the property being tested and the conditions under which the result is obtained.
09Applications in Windows, Doors, and Curtain Walls
Reinforced polyamide profiles are used in a range of architectural aluminum systems. The section design and mechanical requirements vary with the frame structure, opening configuration, and assembly process.
Aluminum Windows
In thermally broken window frames and sashes, the strip separates interior and exterior aluminum sections. Its cross-section must match the frame and sash cavities while maintaining suitable engagement during assembly. Window system designers also consider frame depth, glazing arrangement, weather sealing, and drainage.
Aluminum Doors
Door profiles may experience repeated operation and mechanical loading around hinges, locks, and connecting sections. The thermal break must fit the aluminum profile and remain stable during fabrication and use. The complete door design determines the required section geometry and mechanical specification.
Curtain Wall Systems
Curtain wall framing commonly includes vertical mullions and horizontal transoms. Thermal break sections are incorporated into compatible aluminum components to separate interior and exterior metal parts. Profile dimensions, connection details, and structural requirements need to be considered together.
Other Architectural Aluminum Profiles
Special architectural extrusions may use non-standard cavity shapes or dimensions. In these cases, a profile developed around the extrusion drawing can help address specific engagement and separation requirements. The design process should include the aluminum geometry and the assembly method from the beginning.
Window Frames and Sashes
Used between compatible interior and exterior aluminum frame sections.
Door Frame Systems
Designed around the groove structure and mechanical needs of door extrusions.
Curtain Wall Mullions
Applied in vertical framing sections with suitable thermal break cavities.
Curtain Wall Transoms
Matched to horizontal aluminum sections and their assembly requirements.
10Customized Profile Development and Technical Coordination
Not every aluminum extrusion uses a standard thermal break geometry. A customized profile may be needed when the cavity dimensions, locking structure, or required separation differ from commonly used sections. The development process should begin with a clear understanding of the receiving aluminum profile.
Information for Profile Evaluation
An aluminum extrusion drawing is a useful starting point because it shows the cavity and locking details that determine the required profile shape. Dimensional information should identify critical widths, heights, wall sections, groove openings, and tolerances.
It is also helpful to define the intended assembly method, production equipment, required strip length, and any special appearance or packaging requirements. These details reduce uncertainty during profile evaluation and tooling development.
Typical Customization Options
- Cross-section: I-Type, C-Type, T-Type, or a special-shaped design.
- Dimensions: Customized width, height, thickness, and locking details.
- Color: Color selection according to the agreed material and production specification.
- Length: Straight-cut lengths or suitable coiled supply forms.
- Identification: Laser marking where required by the product specification.
- Packaging: Packaging arrangements suited to storage, transport, and production handling.
Development Workflow
- Drawing review: Review the aluminum cross-section, dimensions, and locking geometry.
- Profile assessment: Confirm the required strip section and identify critical matching dimensions.
- Tooling preparation: Develop or adjust the extrusion die for the specified cross-section.
- Trial extrusion: Evaluate the formed profile and review its dimensional characteristics.
- Dimension confirmation: Check the profile against the agreed drawing and technical requirements.
- Production arrangement: Confirm the final specification, inspection requirements, and supply form.
Technical coordination should continue through the development stages. If insertion is difficult, cracking occurs, or shear strength is insufficient, the investigation may need to consider material condition, profile geometry, groove dimensions, and assembly parameters together.
11A Practical Selection Checklist for Manufacturers
Product selection is more reliable when material requirements and aluminum profile details are reviewed as one specification. The following checklist can help engineering and purchasing teams organize the information needed before confirming a profile.
Material and Reinforcement
- Confirm the PA66 base material and the specified 25% glass-fiber reinforcement.
- Review material condition and relevant processing information.
- Identify the mechanical properties required for the intended assembly.
Profile Geometry and Dimensions
- Confirm the cross-sectional type and all critical dimensions.
- Compare the strip geometry with the aluminum cavity and groove structure.
- Define dimensional tolerances for the features that control fit and locking.
Manufacturing and Quality Requirements
- Review extrusion consistency and dimensional inspection arrangements.
- Identify applicable mechanical, thermal, and environmental test requirements.
- Confirm finished-product inspection and reporting expectations.
Application and Supply Details
- Identify whether the profile is intended for windows, doors, curtain walls, or another aluminum system.
- Specify the insertion or roll-forming process used by the aluminum profile manufacturer.
- Confirm required lengths, supply form, packaging, and product identification.
PA66 GF25 Thermal Break Strips should ultimately be selected according to the technical requirements of the aluminum system. A material designation is an important starting point, but successful integration depends on the relationship between compound properties, cross-section, dimensional accuracy, and assembly conditions.
12Frequently Asked Questions
What does PA66 GF25 mean?
PA66 refers to polyamide 66, an engineering thermoplastic. GF25 indicates that the compound contains 25% glass fiber by weight. The reinforcement increases rigidity and supports dimensional stability compared with an unreinforced PA66 compound.
Why is glass fiber added to polyamide thermal break profiles?
Glass fiber reinforces the polymer matrix and improves stiffness and dimensional control. These characteristics are useful when the profile must maintain its cross-section and withstand forces during insertion, rolling, and handling.
What is the main function of a thermal break strip?
It separates interior and exterior aluminum sections and interrupts the direct conductive path through the metal frame. The performance of the finished system also depends on frame geometry, glazing, seals, and installation details.
What is the difference between I-Type, C-Type, and T-Type profiles?
They have different cross-sectional geometries designed for different aluminum cavity structures. I-Type profiles are generally straight-sided, C-Type profiles use curved or stepped engagement geometry, and T-Type profiles have a head-and-stem configuration. Compatibility must be confirmed against the actual extrusion drawing.
How can manufacturers confirm the correct strip dimensions?
Review the aluminum profile drawing and compare cavity width, depth, groove structure, locking details, and required separation with the proposed strip cross-section. The intended insertion or rolling process should also be considered.
Which applications use reinforced polyamide thermal break profiles?
Common applications include thermally broken aluminum windows, doors, curtain wall mullions, transoms, and other architectural aluminum extrusion systems. The required profile depends on the cavity design and mechanical requirements of each system.
What tests are relevant to thermal break strip quality?
Depending on the specification, evaluation may include density, Shore hardness, longitudinal and transverse tensile strength, water resistance, thermal aging, linear expansion, dimensional inspection, and surface checks. Test methods and acceptance criteria should be agreed in advance.
Can special-shaped profiles be developed?
Yes. A special-shaped section can be developed around the aluminum profile drawing and its critical dimensions. The development process typically includes profile review, tooling preparation, trial extrusion, dimensional confirmation, and production specification approval.
Are straight and coiled supply forms available?
Supply form depends on the profile geometry and specification. Straight strips may be supplied at 6 meters per piece, while suitable profiles can be supplied in 500-meter rolls. The appropriate form should be confirmed for the selected section.
What information should be prepared before requesting a quotation?
Prepare the aluminum profile drawing, required strip dimensions, cross-section details, material specification, assembly method, target length, and any inspection or packaging requirements. These details help clarify the technical scope before production is arranged.
Looking for a Thermal Break Profile That Fits Your Aluminum System?
Share your aluminum profile drawing, required dimensions, and assembly details to discuss a suitable polyamide section. Our team can help review the cross-section, material specification, and technical requirements for your application.
Contact us to Discuss Your RequirementsTechnical coordination for aluminum windows, doors, curtain walls, and customized extrusion profiles.
Manufactured by Jinxing · Reinforced Polyamide Thermal Break Profiles